 EN
 Deutsch
 Español
 Français
 Italiano
 Português
 Nederlands
 Polski
 Bahasa Indonesia
 Русский
 Українська
 العربية
 עברית
 日本語
 한국어
Why Real-Time Manufacturing Dashboards Fail to Show Production Flow
By Mirko Peters ·
Discover why real-time manufacturing dashboards fail to explain production bottlenecks and how shifting to a live value stream model delivers true operational intelligence.
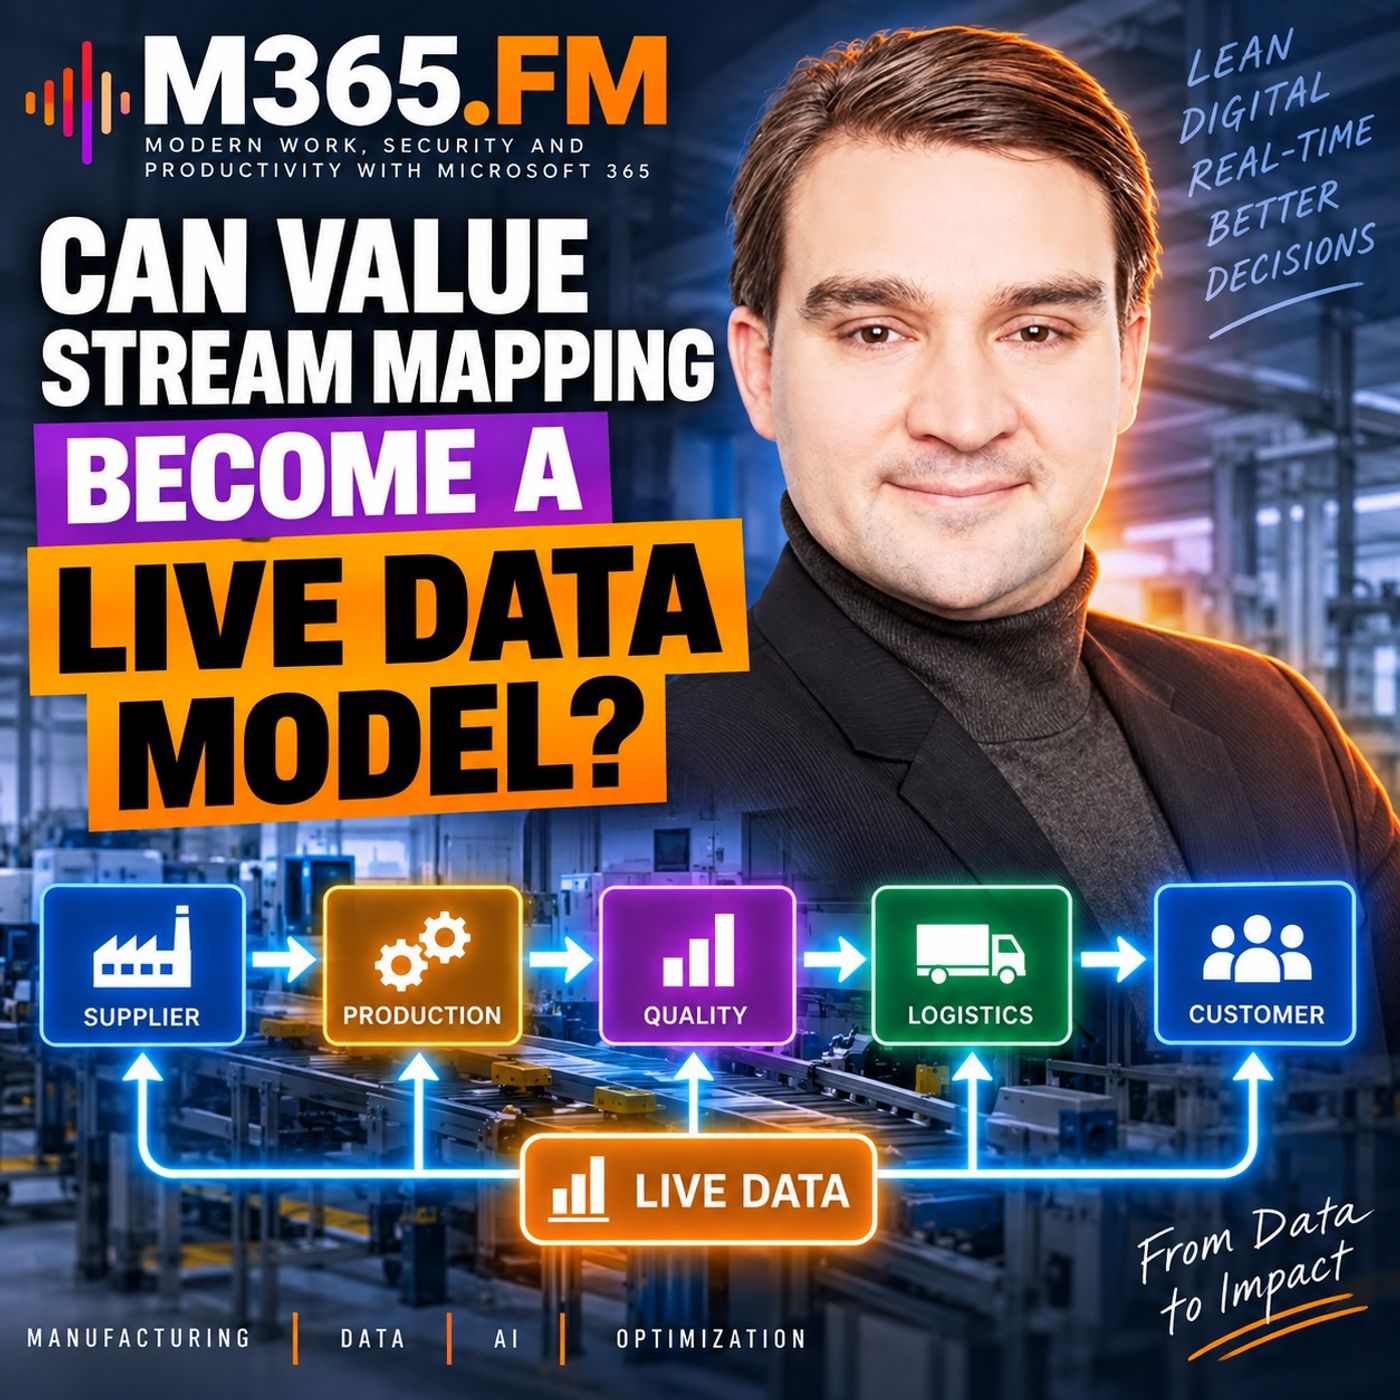
Real-time manufacturing dashboards often create a false sense of operational security by displaying blinking machine tags, open order counts, and active KPI metrics, yet they frequently fail to explain why production bottlenecks occur or where order lead time actually disappears on the shop floor.
Key Takeaways
- Real-time dashboards display machine states and KPI metrics, but they fail to explain the underlying relationships causing production bottlenecks.
- Manufacturing data is scattered across ERP, MES, quality systems, and maintenance platforms, hiding the true path of order lead time.
- Knowing that a machine is idle does not reveal why material is waiting or which upstream constraint blocked the workflow.
- Connecting IT and OT requires a governed semantic process model, not just a faster data lakehouse refresh rate.
- True operational intelligence requires mapping the flow of work, handoffs, and business rules rather than simply presenting a blinking screen of machine tags.
The Illusion of Factory Visibility
Modern industrial digital transformation projects frequently start with a clear objective: give plant managers better visibility into factory operations. IT and OT teams ingest massive streams of telemetry into cloud lakehouses, configure industrial gateways, and construct sophisticated Power BI reports. Within weeks, plant supervisors have access to live dashboards showing machine states, cycle counts, and open production orders.
Yet, when a critical customer order ships late, the plant manager faces a frustrating paradox. The dashboards are running smoothly, every machine tag is reporting its status, and yet nobody can answer a simple question: Where did the lead time actually go?
The core limitation is that a dashboard shows information, whereas a true manufacturing model describes relationships. Knowing that a specific machining center is currently idle does not tell a planner why a batch of material is sitting in a buffer zone three bays away. Visibility without context simply shifts the burden of connecting the dots from physical whiteboards to digital screens, leaving operators and planners to piece together the truth across disconnected systems.
Why Dashboards Miss the Flow
Manufacturing environments are complex ecosystems where business systems and operational floors speak entirely different languages. To understand why standard dashboards fall short, we must examine how data fragments across enterprise platforms and why isolated telemetry cannot reveal production flow.
The Siloed Nature of Manufacturing Systems
Consider a typical make-to-order manufacturing plant. Customer demand enters through an Enterprise Resource Planning (ERP) system, which generates sales orders, verifies material availability, and assigns a planned routing. Down on the shop floor, a Manufacturing Execution System (MES) dispatches work orders and records operator confirmations. Meanwhile, industrial IoT sensors and Programmable Logic Controllers (PLCs) track equipment run states, furnace temperatures, and test station results.
Each system captures an essential slice of the manufacturing reality. However, none of them possesses the complete picture:
- ERP knows when an order was promised, but its routings represent expected theoretical flows rather than physical shop floor realities.
- MES tracks operation confirmations, but it often lacks granular visibility into maintenance constraints or quality hold transactions occurring outside the immediate work cell.
- Quality systems record non-conformances and inspection sign-offs, but release transactions often occur hours after physical inspection is complete, keeping material trapped in administrative limbo.
- Maintenance systems log scheduled service tasks, yet a machine may appear fully available in planning software while unrecorded mechanical tweaks keep it offline.
The Trap of More Telemetry
When visibility projects fail to diagnose delays, the common engineering reaction is to collect more data. Teams connect additional sensors, pull high-frequency historian logs, and add more widgets to existing executive screens. But flooding a data lake with high-frequency machine signals does not automatically create a live value stream.
If an operator confirms a batch at the end of a shift rather than at the exact moment of physical completion, the underlying database records a false timestamp. A dashboard ingesting this data will display a clean, automated report based on corrupted sequence logic. Faster refresh rates cannot repair missing handoff records or undefined operational states; they merely present inaccurate process assumptions with greater frequency.
Moving from Dashboards to Live Models
Overcoming the limitations of traditional dashboards requires shifting the architectural goal from displaying real-time tags to modeling operational relationships. A live manufacturing model treats production as an interconnected web of orders, materials, resources, quality states, and business rules.
Instead of asking "What is the current status of Machine A?", a model-driven approach asks disciplined flow questions:
- Where is this specific order physically located right now?
- What exact event proves that the previous operation has truly finished?
- Which resource is required next, and is it actually unconstrained by maintenance or staffing?
- Is the order waiting because of a physical bottleneck, or because an information delay is blocking the release?
By connecting the foundational logic of traditional lean manufacturing analysis with live event data from ERP, MES, and quality platforms, manufacturers can build a semantic layer that bridges Information Technology and Operational Technology. This transforms static wall charts into dynamic operational models that adapt as reality changes.
Conclusion
Real-time manufacturing dashboards have tremendous value for monitoring isolated assets, but they cannot replace the structural insight needed to optimize end-to-end production flow. By moving beyond simple visibility screens and building connected data models that reflect true operational relationships, organizations can finally answer where lead time goes and how to eliminate hidden plant floor waste.
To dive deeper into how modern manufacturers are bridging IT and OT systems to evolve beyond static documentation, Listen to the full episode and subscribe to the podcast for more practical insights into enterprise cloud and manufacturing architectures.
Frequently Asked Questions
Why do real-time manufacturing dashboards fail to prevent production delays?
Real-time dashboards show current machine states and open order counts, but they lack relational context. While a dashboard can tell you a machine is idle, it cannot automatically explain whether the cause is a missing operator, a quality hold, a lack of raw material, or an upstream scheduling queue.
What is the difference between visibility data and a live value stream model?
Visibility data displays isolated operational metrics and KPI counts in a lakehouse or Power BI report. A live value stream model understands the structural relationships between orders, operations, resources, quality holds, and material constraints to continuously track actual production flow.
How do ERP and MES systems differ in tracking shop floor reality?
ERP systems manage business orders, material requirements, and planned routings, which represent how production is supposed to happen. MES platforms track shop floor execution, operator confirmations, and work order progress. However, neither system alone captures the complete cross-functional reality of why an order experienced a delay.
Does a live manufacturing model require second-by-second data updates?
No. A live model should refresh at the pace of the decision it supports. While certain emergency events like critical machine faults or quality holds require rapid attention, standard operational planning and continuous improvement reviews rely on consistent event definitions and contextual completeness rather than constant rapid telemetry.